Understanding Fatigue Why disc springs crack, and how to estimate their life
Subtle and unappreciated, metal fatigue has been the root cause of many a disaster. From experience we know that fatigue is often overlooked in engineering designs, and consistent, predictable performance and behaviour are lost.
As part of our Quality Management System and Value Proposition, we have a design and manufacturing risk assessment that, from once being an internal QA input, now sees us spending time in the heart of our customers’ operations. Very often, we find issues where the root cause is metal fatigue.
Fatigue occurs when the base metal of a structure or component becomes weak from repeated stress cycles. Metal fatigue begins with crack initiation (imperceptible to the naked eye) and its subsequent propagation due to the cyclic loading and unloading.
Those who have chipped a windscreen know the inevitability of the process, as they watched the slow march of the developing crack, that might take weeks to develop and finally fail. But fail it always does!
Ubiquity of Fatigue
It is not unusual for us to pick up an issue in the operations of our customers by taking note of the frequency with which a particular size is ordered, the number of spares required, or the frequency of urgent breakdowns.
In these instances, when we conduct an investigation, we invariably find disc springs being applied in a sub-optimal manner. The point to note is that without exception, metal fatigue has been either the root cause or a contributing factor, and hence the focus of any remediation.
When we investigate, we join our customer’s plant managers and maintenance teams, dismantle machines in situ (this can be a messy business!) and conduct our failure analysis. This includes:
- an analysis of the disc springs themselves: material composition, hardness and hardening, contact flats, radii, dimensions, etc.
- the installation of the disc springs: clearances, alignment, lubrication, etc.
- the actual physical dynamics of the stack: preload, final design load, travel, etc.
- a verification of the engineering design: stresses, loads, etc.
So by being curious and caring about our customers, we ask the right questions, provide solutions and add great value by 1) greatly reducing unscheduled downtime, 2) reducing waste and rework, and 3) reducing maintenance costs.
To reiterate and emphasise the point: metal fatigue is always either the root cause or a contributing factor, and must be the focus of any remediation.
The intention of this page is thus to:
- Build awareness with our customers of the importance of understanding fatigue
- Introduce some concepts that are useful in understanding the problem
- Provide some tools that allow us to quantify objectively consistent and predictable operating lifespans
- Explain some of the gaps, shortcomings and consequences that manufacturers conveniently neglect to share regarding fatigue
- Differentiate ourselves from the rest of the market
Useful Concepts & Terminology
Elasticity
The tendency of solid objects and materials to return to their original shape after the external forces (load) causing a deformation are removed. An object is elastic when it returns to its original size and shape when the load is no longer present. Elastic behaviour varies vastly between materials and depends on the microscopic structure of the material.
Plasticity
Behaviour that occurs when stress is greater than the material’s elastic limit. In the plastic region, the object or material does not return to its original size and shape when the loading stress is removed, but instead acquires a permanent deformation. Plastic behaviour ends at the breaking point.
Yield strength
The stress at which plastic deformation starts to occur as the material is loaded. There is no definite point on the curve where elastic strain ends and plastic strain begins, so the yield strength is taken as the stress at which a definite amount of plastic strain has occurred, normally 0.2%. This 0.2% offset yield strength (Rp0.2) is found by drawing a line parallel to the elastic part of the stress–strain curve, offset by 0.2% strain. As with stress, which we denote with the Greek small letter sigma (σ), yield strength is measured in MPa or N/mm2.
Strain
The deformation of a material caused by stress. It is simply a ratio (so it appears as a % on graphs) of the change in length to the original length. Deformations perpendicular to the cross-section are normal strains, while deformations parallel to the cross-section are shear strains.
Stress
The applied force F (or load) divided by the cross-sectional area: “force per unit area”. Tensile stress tends to stretch or lengthen the material and acts normal to the stressed area, whilst compressive stress tends to compress or shorten the material. We denote the difference between the two by a positive (tensile) or negative (compressive) sign.
Base material
We purposefully use spring steels in the manufacture of disc springs because of their physical and mechanical properties of durability, pliability, toughness and longevity (once heat treated properly!). All of these properties relate to the spring’s ability to react to loading by elastic deformation. Where requirements such as non-magnetism, elevated operating temperatures or highly corrosive environments require alternative materials, the published product data, which relates to spring steel, should not be used. For more on this subject, please see our detailed discussion on materials used in the manufacture of disc springs.
Stress–Strain Diagrams
We can graph the relationship between stress and strain on a stress–strain diagram. Each material has its own characteristic stress–strain curve.
In the diagram, the curve is linear between O and A, so Hooke’s Law holds in this region. From A to B, stress and strain are no longer proportional, but if we remove the load, the body still returns to its original dimensions.
Point B is the yield point or elastic limit, and the corresponding stress is the yield strength (Sy) of the material. Once the load is increased further, the stress exceeds the yield strength and the strain increases rapidly, even for a small change in stress.
This is shown in the region from B to D. If the load is removed at, say, point C between B and D, the body does not regain its original dimensions. Even when the stress is zero, the strain is not zero; this is plastic deformation.
Point D is the ultimate tensile strength (Su) of the material. If any additional strain is produced beyond this point, fracture can occur (point E). Note that:
- if the ultimate strength and fracture points (D and E) are close together, the material is brittle;
- if they are far apart, the material is ductile.

Estimating Fatigue
The key points on a disc spring where stress must be considered are, by convention, referred to as σI to σIV, as shown in Fig 2. Of these, our product lists give σI to σIII.
The tensile stresses at points σII and σIII, on the underside of the disc, are used to estimate disc spring fatigue life, because this is where fatigue cracks originate. The compressive stress σI at the top inner edge matters for static loads and setting (relaxation), not for fatigue.
To estimate fatigue life, work out σII and σIII at the preload (lower stress σU, at deflection s1) and at the final design load (upper stress σO, at s2). The point with the larger stress range σh = σO − σU governs, and its σU and σO are plotted on the fatigue diagram.

The DIN EN 16983 rules in short
- Minimum preload. Install every dynamically loaded spring with a preload of at least s1 ≈ 0.15 to 0.20 × h0. Below this, the residual tensile stress left near point I by pre-setting can start cracks there.
- Three diagrams, chosen by thickness: t < 1.25 mm, 1.25 mm ≤ t ≤ 6 mm and 6 mm < t ≤ 14 mm. These match Groups 1, 2 and 3. Discs thicker than 14 mm are not covered.
- Life lines are given for 105, 5 × 10⁵ and 2 × 10⁶ cycles. A spring that reaches 2 × 10⁶ cycles is regarded as fatigue resistant (endurance). Below 105 cycles the diagrams give no estimate.
- Material and finish. The diagrams are for shot-peened discs made of the spring steels in EN 16983 (for example C60S, C75S, 51CrV4), hardened and tempered. They are not valid for stainless, heat-resistant or non-ferrous materials, or for discs that are not shot peened.
- Stacks. The diagrams are for single discs and short stacks. In long stacks (more than about 10 discs in series) and parallel stacks, friction and uneven deflection shorten the life, so allow a margin.
- Use them as an estimate. They give a 99% survival probability under ideal conditions. Corrosion, high temperature, impact loading or poor guidance all shorten the life.
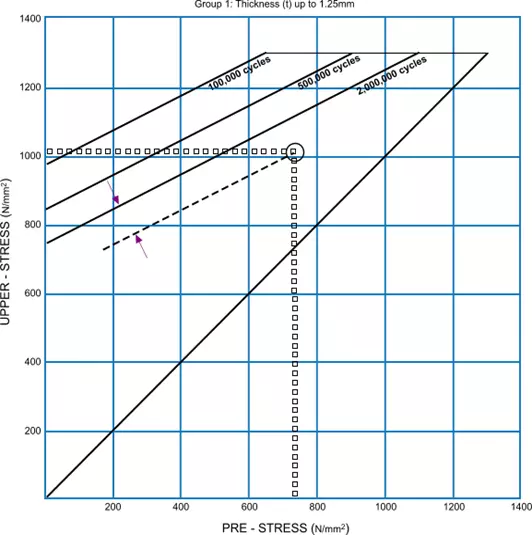
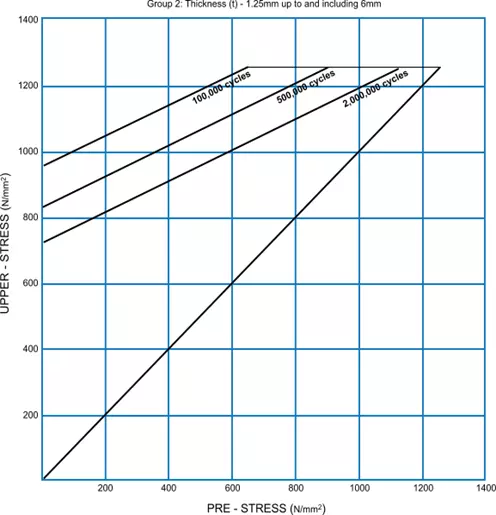
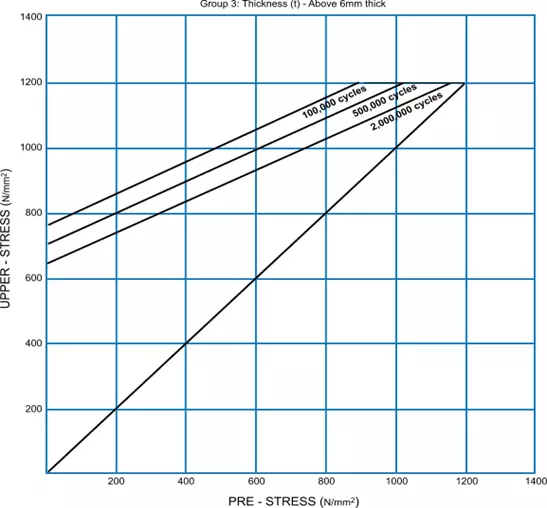
To use a diagram, draw a vertical line from the X axis at the lower stress σU (preload) and a horizontal line from the Y axis at the upper stress σO (final design load). Compare where the two lines meet with the nearest life lines; this is the estimated fatigue life.
Reading a Goodman Diagram
There is a lot to interpret in a fatigue (modified Goodman) diagram, and Fig 4 attempts to make it all clear.
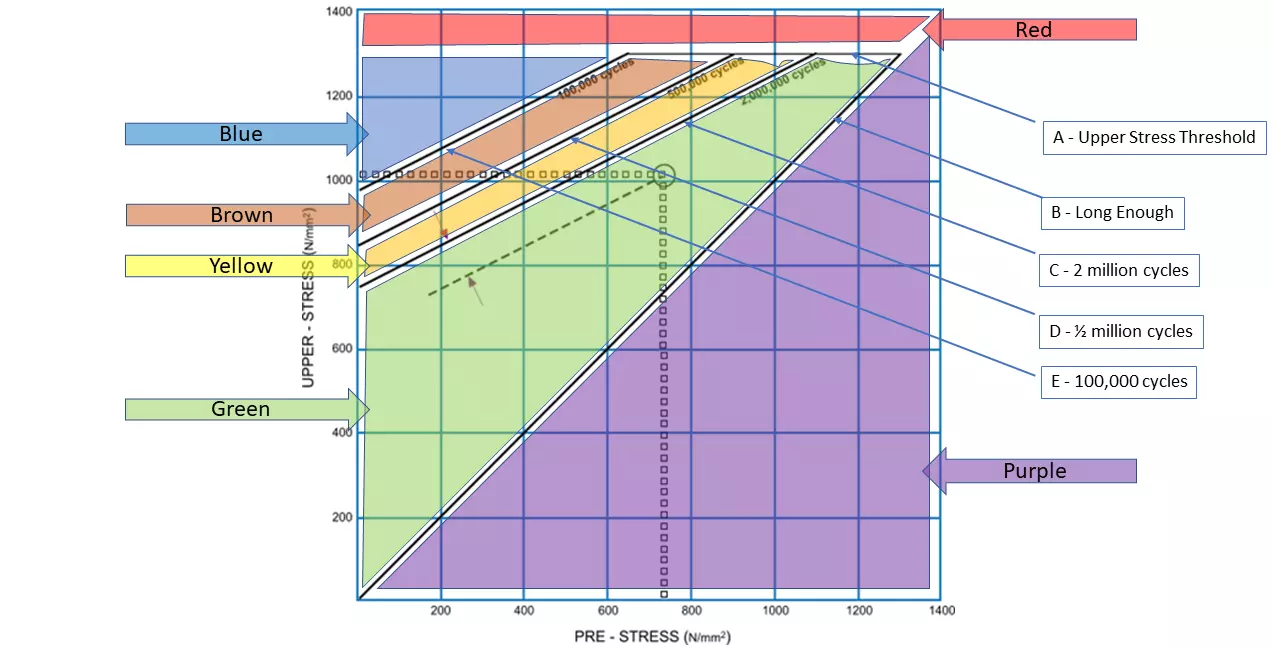
The diagram has six regions (red, blue, brown, yellow, green and purple), bounded by lines A to E.
It is important to note:
- There is a separate diagram for each thickness range (Groups 1, 2 and 3).
- There are no diagrams published for disc springs made of anything other than spring steel.
- The diagrams are not strictly valid for stacks of more than about 10 discs in series (i > 10) or with more than 2 discs in parallel (n > 2).
Worked Example
Let’s estimate the fatigue life of a Series B, Group 2 disc spring with an outside diameter of 50 mm, an inside diameter of 25.4 mm, a thickness of 2 mm and a free height of 3.4 mm (h0 = 1.4 mm). The preload is 15% of h0 and the final position is 75% of h0.
| s | σII | σIII | |
|---|---|---|---|
| Preload, 15% of h0 | 0.21 mm | 128 MPa | 264 MPa |
| Final load, 75% of h0 | 1.05 mm | 923 MPa | 1,140 MPa |
| Stress range σh | 795 MPa | 876 MPa |
The largest stress range is at point III, so we use σU = 264 MPa and σO = 1,140 MPa. The disc is 2 mm thick, so we use the Group 2 diagram (Fig 3b).
Draw the vertical line at 264 MPa and the horizontal line at 1,140 MPa. They meet above the 100,000 cycle line, which sits at about 1,080 MPa for this preload. The estimated life is less than 100,000 cycles, outside the range the diagram covers, so this spring is not suitable for this dynamic duty. Reducing the final deflection, or choosing a thicker or larger disc, brings the point down into the brown, yellow or green region.
Reality Check
Do not assume that all disc springs on the popular commercial lists are equal. It is amazing to see how mistakes made on one list manage to migrate across the world to other businesses. Someone is having a laugh! Mistake or malicious intent? The point that should sober you up is that there are legacy disc springs on the commercial lists that need to be used with caution. This is why we show a red flag on our product lists, and a single star to subtly indicate our views, based on our observations and experiences.
The product data we provide with each disc spring is useful and should be carefully considered when selecting a disc spring. But do not rely on data that appears on any list (not even ours); verify it yourself using our online calculation tool for disc spring stresses and loads.
| 127×250×10 ★ | 127×250×12 🚩 | 127×250×14 🚩 | 127×250×16 🚩 | |
|---|---|---|---|---|
| Series | B | bespoke | A | A |
| t / t′ (mm) | 10 / 9.4 | 12 / 11.25 | 14 / 13.1 | 16 / 14.9 |
| l0 / h′0 (mm) | 17 / 7.6 | 19.3 / 8.05 | 19.6 / 6.5 | 21.8 / 6.9 |
| De/t′ h′0/t′ | 26.6 0.74 | 22.22 0.65 | 19.08 0.43 | 16.78 0.39 |
| s/h′0 = 25% | ||||
| Load | 55,375 N | 95,559 N | 106,973 N | 167,125 N |
| σI / σII / σIII (MPa) | −907 / 182 / 507 | −1110 / 282 / 617 | −939 / 387 / 513 | −1125 / 491 / 612 |
| s/h′0 = 75% | ||||
| Load | 124,945 N | 226,324 N | 281,589 N | 445,829 N |
| σI / σII / σIII (MPa) | −2411 / 856 / 1325 | −2979 / 1204 / 1627 | −2576 / 1396 / 1384 | −3097 / 1743 / 1660 |
| s/h′0 = 100% (flat) | ||||
| Load | 149,428 N | 276,384 N | 359,020 N | 571,210 N |
| σI / σII / σIII (MPa) | −3008 / 1349 / 1634 | −3734 / 1841 / 2018 | −3275 / 2016 / 1744 | −3946 / 2501 / 2097 |
Let’s look at the last column above, a 127×250×16 reduced-thickness disc spring with contact flats. This is a popular disc spring used in a specific generation of arc furnace applications. They are used in stacks of 14 in series to hold in place the crucible, which contains more than 500 tons of molten ore.
Now, what preload to final design load working range can these disc springs accommodate under a dynamic load? You can verify with the tools provided that this seemingly robust disc spring, weighing in at about 4.7 kg, cannot be used in any dynamic application beyond 50% of s/h′0. And you thought that 75% was the recommended limit! Even at 50%, with a 15% preload, σIII goes from about 373 to 1,163 MPa, which is already above the 100,000 cycle line of the Group 3 diagram. At 16 mm it is also thicker than the 14 mm the DIN fatigue diagrams cover.
Ok, then what of a static load? Look at the stress at point I, which hints that this is a disc spring that, if not properly manufactured, will experience relaxation and setting within hours of use. That becomes a problem when it is installed on an arc furnace, where every hour of downtime costs $$$$!
There are other monsters lurking in the lists out there. Be careful, and let us help you.
Worried about fatigue in your machine?
Send us your application, stack and loads. We’ll check the stresses and fatigue life and recommend the right disc spring.